Lead-free solder paste for fine-pitch parts
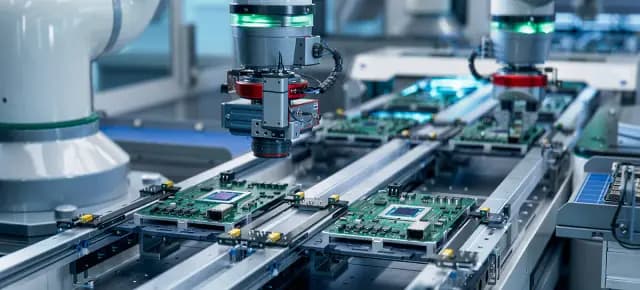
Lead-free solder paste with fine type 5 powder helps reduce bridging and insufficient solder when assembling 0201 and 01005 components and fine-pitch BGAs, keeping pace with the miniaturization of electronic devices.
As component lead pitch shrinks to 0.4 mm or less, stencil apertures shrink as well. Coarse-powder solder paste cannot pass through the apertures consistently, resulting in unstable printed solder volume, which causes bridging where there is too much and open joints where there is too little.
According to widely cited SMT industry statistics, most soldering defects originate in the paste printing step. Choosing the right solder paste is therefore the most effective way to raise first-pass yield.
Solder paste powder size classification
| Type | Particle size | Application |
|---|---|---|
| Type 3 | 25–45 µm | Standard components, 0.5 mm pitch and above |
| Type 4 | 20–38 µm | 0402 components, 0.5 mm BGA |
| Type 5 | 15–25 µm | 0201 components, 0.4 mm BGA |
| Type 6 | 5–15 µm | 01005, SiP, high-density packaging |
The five-ball rule
Practical experience shows that the smallest aperture width should accommodate at least five solder powder particles side by side. With a 100 µm aperture, type 5 paste meets this rule well, while type 3 does not.
Considerations when switching to fine-powder paste
Stencil aperture area ratio
The ratio of aperture area to aperture wall area should be greater than 0.66. A thinner stencil of 80–100 µm, or a laser-cut electropolished stencil, may be needed.
Oxidation and stencil life
Fine powder has a large surface area and oxidizes more easily. Choose a paste with a suitably active flux system, limit paste time on the stencil and solder in a nitrogen atmosphere if possible.
Solder balling
Fine-powder paste tends to form small solder balls around components. Adjusting the reflow profile and reducing the initial ramp rate helps limit this.
- Store paste at 2–10°C and thaw for 4 hours before opening.
- Inspect print volume with SPI on 100% of boards.
- Wipe the stencil periodically based on print count.
Not every board needs fine-powder paste. On mixed-technology boards, many plants choose type 4 as a compromise, or use step stencils to print different solder volumes for large and small components. DOE trials with several stencil and paste options will help find the optimal configuration for each product.
AMS supplies lead-free solder paste in multiple powder grades along with support for reflow profile optimization. Contact AMS Vietnam for advice.