SMT adhesives holding parts before wave soldering
SMT red glue is dispensed or printed onto the board before component placement, then heat cured to hold components firmly on the bottom side. As a result, when the board is flipped over and passes through the wave soldering machine, components do not fall off or shift out of position.
This mixed-technology process is still common for power supply boards and home appliance control boards with many through-hole components. Understanding the properties of SMT adhesives helps reduce dropped-component defects and glue contamination on pads.
How SMT adhesives work
SMT adhesives are usually one-part epoxies with thixotropic rheology: viscosity drops under shear during dispensing and recovers immediately when it stops, so the dots keep a tall profile without spreading. The red or yellow color makes them easy for AOI cameras to detect. The adhesive cures at about 120–150°C in 60–120 seconds, compatible with a reflow oven or a separate curing oven.
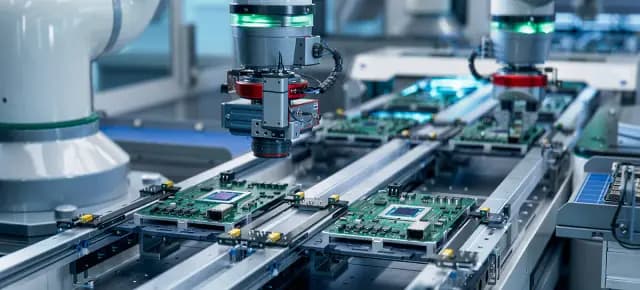
Dispensing vs. stencil printing
There are two main methods for applying adhesive to the board:
- Dispensing with a dispensing machine: flexible, easy to reprogram, suitable for high-mix production.
- Stencil printing: high throughput, suitable for high-volume production with few design changes.
- Non-contact jetting: high speed and uniform dots, but a larger equipment investment.
Requirements for adhesive dots
The dot height must be greater than the distance from the board surface to the component body, while not spreading onto the solder pads. For 0603 components, the dot diameter is about 0.4–0.5 mm; SOIC components need two to three dots distributed under the body.
Common defects
- Stringing: usually caused by excessive viscosity or incorrect needle height; adjust the adhesive temperature and needle retract speed.
- Adhesive on pads: too much adhesive or misplaced components, resulting in insufficient solder joints.
- Weak holding force: insufficient cure; check the actual thermal profile at the adhesive location.
- Voids in the dots: the adhesive absorbed moisture after being left out of the refrigerator too long.
To evaluate cure, many plants use a component push-off test after the oven, with a minimum force depending on size, for example above 1.5 kgf for 1206 components.
Storage and pot life on the machine
SMT adhesives are usually stored at 2–8°C and must be allowed to reach room temperature for at least a few hours before being loaded onto the dispenser. Once opened, the adhesive in the syringe should be used up within the period recommended by the manufacturer. Do not transfer leftover adhesive from an old syringe into a new one, as this easily introduces air bubbles and contaminants, causing inconsistent dots.
AMS distributes Loctite SMT adhesives and equivalent grades, along with dispenser setup guidance. Contact AMS Vietnam to receive samples for your production line.